


Differential voltage in power battery system – the causes and improvements


The importance of power batteries
EV battery cell is one of the three core components of new energy vehicles. The internal integration is complex and usually consists of dozens or even hundreds of cells connected in series and parallel. Therefore, higher consistency requirements are required.
The consistency of power batteries usually refers to the difference between cells, which can be divided into the consistency of the manufacturing process and the consistency of the use process. The consistency of the manufacturing process is mainly related to factors such as manufacturing technology and production control level.
The consistency of the use process mainly depends on system integration and battery management. If there is a problem with the cells in the power battery, such as capacity reduction or leakage, then there will be problems with the voltage difference of the power battery.
As the battery system is used, the voltage difference will further expand. Due to the barrel effect, the cell with the lowest voltage during discharge will reach the discharge cut-off voltage first, and the cell with the highest voltage will reach the charge cut-off voltage first during charging, thus affecting the battery capacity and the driving range of the vehicle.
Today we will introduce the voltage difference of the power battery system. Through big data screening and on-site inspection, the possible causes of the voltage difference are investigated one by one, including cell consistency, manufacturing process, production batch, BMS (Battery Management System) control strategies, hardware and usage habits, and some suggestions to improve the problem.
What is the voltage difference problem of power battery system
The battery system voltage difference problem is prominent. A total of 8,723 vehicles were selected from the big data for statistical analysis. Each vehicle is a sample, and the corresponding battery system will generate a voltage difference value. The voltage difference warning threshold when fully charged is 120 mV, the voltage difference warning threshold is 220mV.
The data of all samples that triggered the voltage difference warning value and voltage difference warning value within 38 consecutive weeks were extracted for analysis. A total of 1099 voltage difference warning data were generated, including 446 voltage difference warning maintenance data.
In order to analyze 1099 samples with abnormal voltage differences, 7624 samples that did not trigger the early warning threshold were randomly selected as controls. The control sample selection conditions were: fully charged and the highest cell voltage Vmax ≥4.2 V.
The voltage difference Vdif when fully charged is calculated as Vdif= Vmax-Vmin
In the formula: Vmax is the highest cell voltage in a single sample when fully charged; Vmin is the lowest cell voltage in a single sample when fully charged.
Analyze a single sample, calculate the Vdif value of a single sample according to the charging date, and obtain the time series Vdif 1, Vdif 2,…, Vdif i,…, Vdif n of a single sample Vdif, where the number of days between dates t must satisfy t≥14 d , n is the number of calculations of the full power voltage difference of a single sample within 38 consecutive weeks.
The voltage difference change rate k’i of a single sample is k’i=(Vdif i+1-Vdif i)/ti
In the formula:
- Vdif i+1 is the calculated voltage difference of a single sample at the i+1 full charge, mV;
- Vdif i is the calculated voltage difference of a single sample at the i-th full charge, mV;
- ti is the two consecutive full charges.
The voltage difference calculation time interval is ti≥14 d; the value of i is 1≤i≤n-1. The time series k’1, k’2,…,k’i,…,k’n-1 of the voltage difference change rate of a single sample is calculated from Equation Vdif, and the average value of the sequence is k’ave. For 8723 samples, 8723 k’ave values were calculated. The k’ave distribution of abnormal samples and control samples within 0~1.25 mV/d is shown in the figure below.

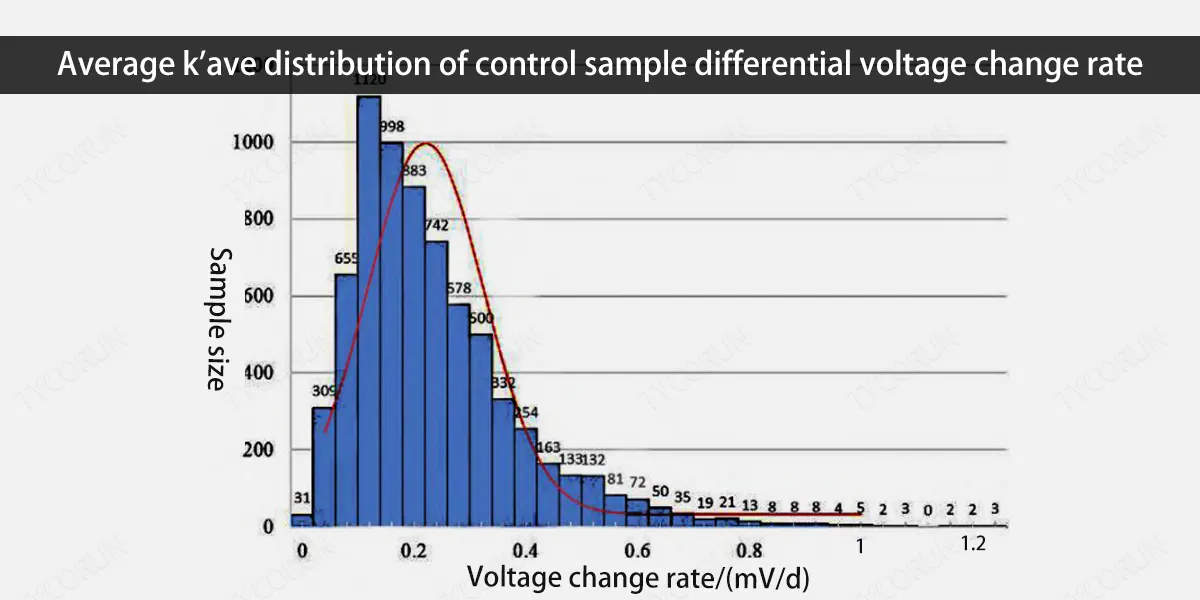
Combining the above two figures, the monthly voltage difference change value of a single sample can be obtained by k’ave , the monthly capacity attenuation value is the monthly self-discharge capacity. The statistical results of all samples in this article are shown in the table below.
Battery cell production process
From the 446 voltage difference warning samples, 3 samples were selected whose self-discharge amount was higher than the battery cell specification requirements and the charge end voltage difference still increased by ≥20 mV/month after manual equalization.
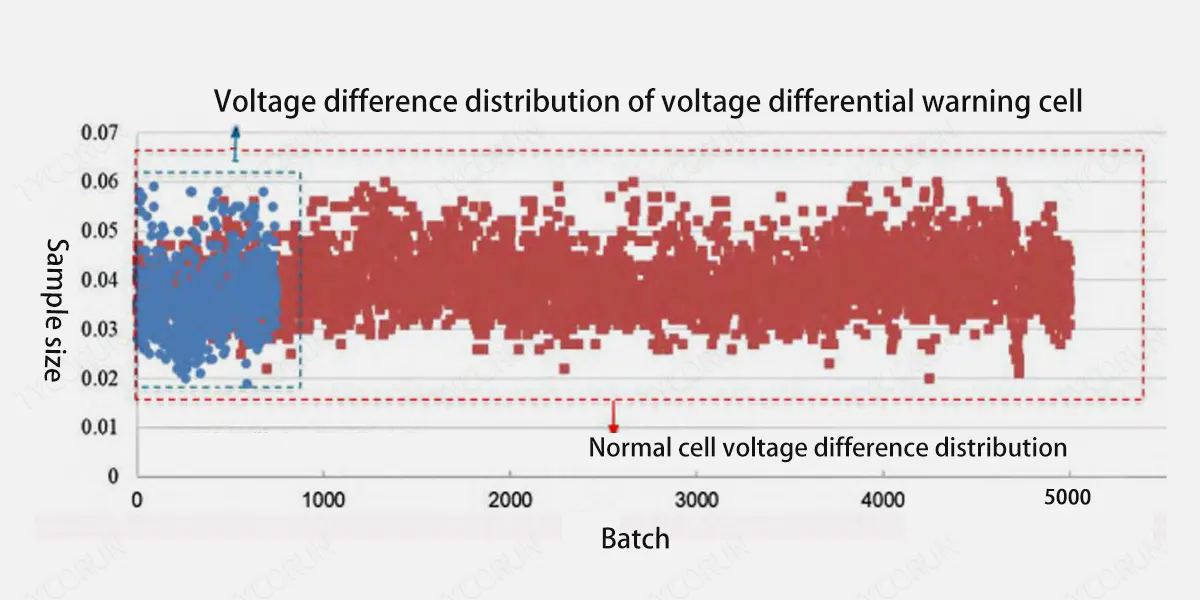
The reason for the high voltage is that there are particles in the core that break through the separator. The particles are composed of iron, chromium, and stainless steel. Therefore, the battery cell production process is one of the reasons for the voltage difference problem in the battery system. Statistical analysis was conducted on the production batches of battery cells in the abnormal samples, and it was found that the battery cells produced in the 13th and 24th weeks had the highest frequency of warnings.
While comparing with the factory voltage difference of the normal batch of battery cells, no abnormality was found, as shown in the figure below, the overlap between the two is relatively high; comparing with the self-discharge test results of the normal batch of battery cells, no abnormality was found. The excellence rate values of each batch are not much different. Therefore, the production batch is not the cause of the cell voltage difference problem.
Comparison of cell voltage differences between different batches:
BMS balancing strategy
Differences in the self-discharge rate (self-discharge capacity/rated capacity) of different cells in each sample are unavoidable. The balancing function must be used to make the cell voltages consistent and make up for the self-discharge rate difference between cells.
The estimated equation for the required equilibrium time is:
The number of balancing hours required per day = cell capacity × self-discharge rate difference of monthly cells / (average balancing current × proportion of balancing on time × 30)
In the formula:
- The cell capacity is the rated capacity of the cell;
- The monthly cell self-discharge rate difference (the difference in cell self-discharge rate between the highest voltage cell and the lowest voltage cell in the sample) is obtained by measurement;
- The average balance current is the rated voltage/balanced resistance of the battery cell;
- The proportion of balanced on time depends on the hardware capability, and the balanced on time of different hardware is different;
- A month is calculated as 30 days.
Based on a monthly cell self-discharge rate difference of 2.5%, this model of battery system requires 4.5 hours of balancing hours per day. According to big data statistics, the daily use time of private electric vehicles is 2 hours, which is less than 4.5 hours. Therefore, the voltage difference of the battery system will gradually increase during use.
Hardware failure
Some vehicles have the problem that the cell voltage in concentrated areas is lower than other string numbers, as shown in figure below. Voltage differences caused by battery cell problems are often discretely distributed. The cell sampling controller is powered by the module. The concentrated and low voltage is mostly caused by BMS hardware abnormalities.
From the picture below we can see that one group of cells has a low voltage:
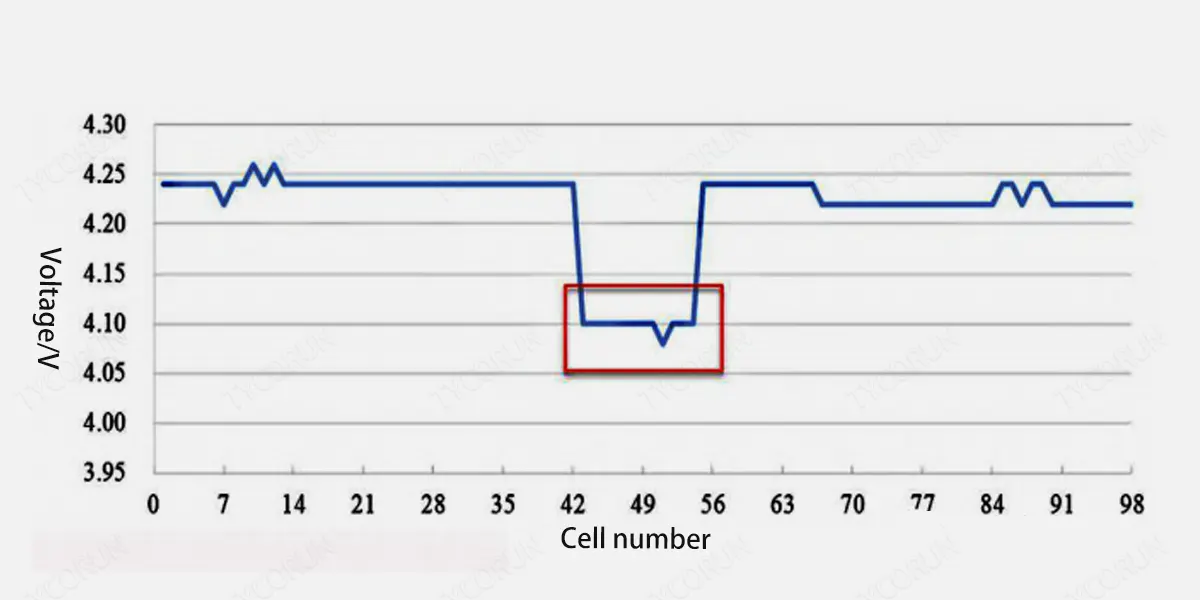
As shown in the figure below, the PIN 17 is directly connected to the optocoupler PIN 4, which is the way in which ESD (Electro-Static Discharge) is introduced. ESD will occur if electrostatic protection is improper during the assembly of the sampling controller or the battery system. When the optocoupler is normal and the low voltage is not powered on, the optocoupler will not turn on and will not power subsequent chips.
When the optocoupler is abnormal, the photocoupler will not turn on due to the MOSFET (Metal-Oxide-Semiconductor Field-Effect Transistor) damage, causing leakage of the optocoupler PIN4 to PIN3, and the subsequent chip operates due to power supply, resulting in abnormal leakage current.

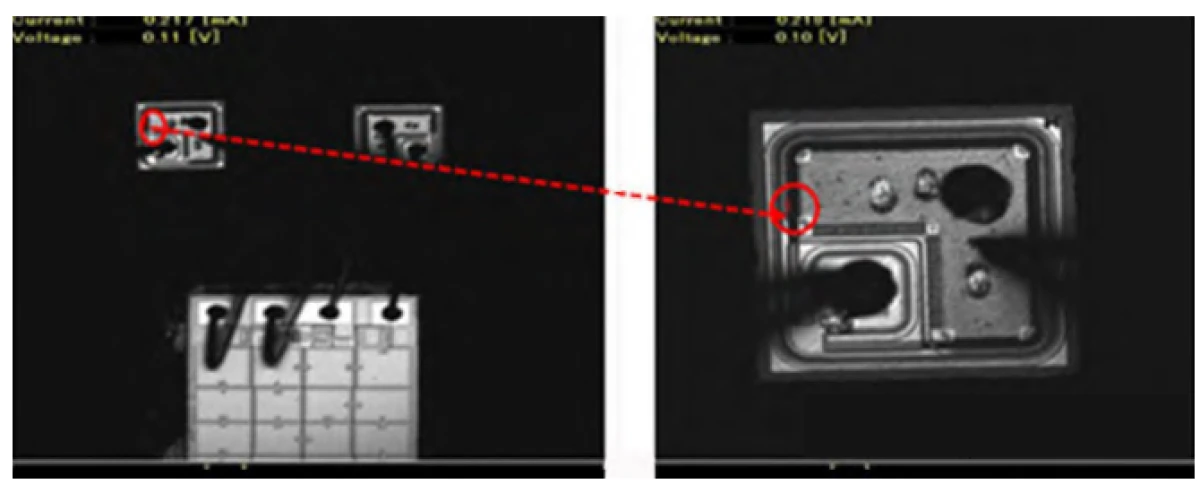
When perform thermal imaging analysis on the failed optocoupler, as shown in the figure below, we can see the failure location. Therefore, the failure of the optocoupler is one of the reasons for the increase in voltage difference.
Optocoupler failure position 1:
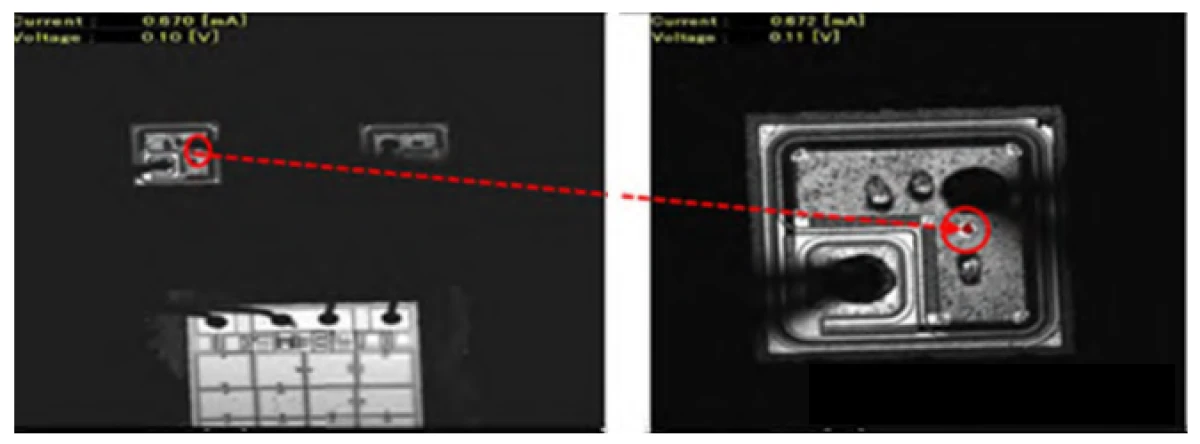 Optocoupler failure position 2:
Usage habits
Different usage habits will affect the charge and discharge rate, and charge and discharge depth of the battery system. A single sample has various usage scenarios and has no analytical value. Comparing the data indicators of abnormal samples and control samples within one year, including charging time, charging start and end SOC (State of Charge), single lithium battery state of charge ΔSOC, as shown in the figure below, the difference between the two groups of samples under each indicator is small, indicating that the usage habits are basically the same.
Therefore, the usage habits have basically no impact on the increase in the voltage difference of the battery system.

Improvement of battery voltage difference
- Optimize the battery production process and establish a market maintenance mechanism:
At the production end, the management of the production environment should be strengthened, the dust removal process should be optimized, so that the possibility of dust mixing can be reduced.
Establish a maintenance mechanism on the market side. For battery systems with a charging end voltage difference ≥50 mV, balanced charging is required, and the balance qualification standard is a charging end voltage difference ≤30 mV. For balanced cells, when the monthly charging end voltage difference increases ≥ 20.72 mV/month, the voltage difference problem needs to be improved through manual balancing maintenance or module replacement.
- Optimize balancing strategy:
The battery cell capacity, monthly battery cell self-discharge rate difference and balancing current are all fixed values. By increasing the balancing on-time, the balancing efficiency can be improved, thereby reducing the problem of voltage difference increase. However, this will increase the BMS temperature rise and over-temperature. High temperature will cause device damage and to harm to lithium battery safety. Therefore, replacing the BMS shell with a metal shell increases heat dissipation and reduces heat accumulation.
- ESD protection and optocoupler replacement:
Check the ESD protection in the production environment and make improvements from the aspects of personnel, equipment, materials, etc.: replace the electrostatic gloves worn by personnel with surface impedance exceeding the standard, replace the electrostatic leather and seats with excessive impedance, and replace the non-anti-static materials. Defective products should be placed in boxes to improve the production environment.
Since the optocoupler cannot improve its ESD resistance in the short term, the optocoupler can only be replaced at present. The area of the replaced chip has increased to 8.18 times that of the previous one, the withstand voltage has increased by 20 V compared with before, and the distance between the MOSFET peripheral protection rings has increased. After that, the vehicle was tracked, and it was found that the voltage difference of the vehicle was within the normal range, and the voltage difference problem was greatly improved.


Leave a comment